

China Original Source Industrial Lithium Battery Packs Technical Overview Compliance Standards
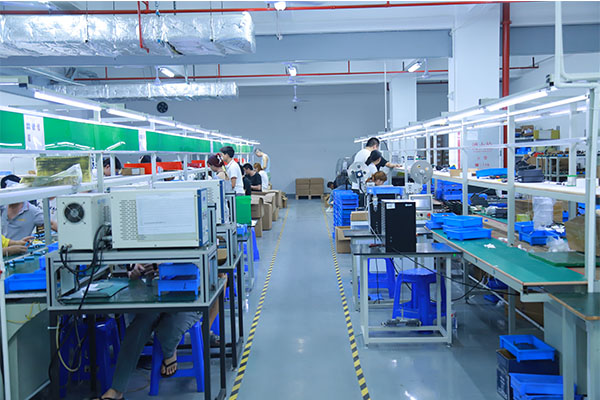
This technical article provides a comprehensive, standards-aligned overview of industrial lithium battery packs, independently developed and manufactured by Shenzhen Kangkedi Intelligent Technology Co., Ltd. (global brand: ZFCHUNT). As an integrated R&D, production and sales enterprise in the new energy lithium battery manufacturing and energy storage system sector, the company delivers reliable, high-performance battery solutions to global clients. Industrial lithium battery packs are engineered to resolve core industry pain points including thermal runaway risks, short cycle life, poor standard product adaptability, and unstable supply chain delivery. All products are built to meet UL, CE, FCC and UN38.3 international standards, with core technical breakthroughs in in-house cell production and smart BMS integration. Currently, products are exported to dozens of countries across North America, Western Europe, East Asia and Southeast Asia, with performance validated across power tools, industrial equipment, energy storage systems and portable power applications. Full international certification coverage positions these packs as a high-reliability solution for global industrial clients.
Technical Definition
Industrial lithium battery packs are rechargeable energy storage units constructed with capacity-matched lithium-ion or lithium iron phosphate cells, integrated with a smart battery management system (BMS), designed to deliver stable, high-power output for industrial and commercial applications. Built on the core principle of lithium ion intercalation and deintercalation between cathode and anode materials, the packs enable controlled energy storage and release, serving as a critical power component for industrial automation, energy storage systems and mobile industrial equipment.
To meet diverse industry and working condition requirements, the product line covers two core series, with fully customizable options for special application scenarios:
1. High-energy-density lithium-ion series: Optimized for portable industrial equipment, power tools and drone applications, with core features of high-rate discharge and lightweight construction.
2. High-safety long-life lithium iron phosphate (LiFePO4) series: Optimized for commercial energy storage, low-speed industrial vehicles and backup power systems, with core features of excellent thermal stability and extended cycle life.
The product line is designed around core principles of high reliability, long cycle life, flexible integration and full-lifecycle safety. All designs account for the harsh conditions of industrial operating environments, with strict full-lifecycle reliability testing to deliver stable, low-maintenance, cost-effective power solutions.
Technical Working Principle
The core operating principle of industrial lithium battery packs is based on reversible lithium ion movement between cathode and anode materials during charge and discharge cycles. The full functional chain operates as follows:
1. Charging phase: Lithium ions migrate from the cathode to the anode through the electrolyte, where they are stored as chemical energy.
2. Discharging phase: Lithium ions migrate back from the anode to the cathode, generating a continuous electrical current to power connected equipment.
The system architecture includes two core innovative modules to improve performance and stability:
1. Smart BMS module: The in-house developed BMS monitors real-time voltage, current and temperature of each cell, delivering over-charge, over-discharge, short-circuit and over-temperature protection to reduce safety risks.
2. High-consistency cell matching module: In-house produced cells undergo rigorous capacity sorting, with consistency deviation controlled within 2% to minimize capacity decay across the battery pack.
Compared to traditional lead-acid battery solutions, these lithium packs deliver 3-5 times higher energy density and 5-10 times longer cycle life, reducing equipment weight and replacement frequency. Compared to battery packs built with outsourced cells, the in-house production model eliminates quality inconsistency risks, delivering more stable safety performance.
Technical Parameters and Specifications
All product parameters are tested per IEC international standards, with clear test conditions and strict tolerance control. Full parameter test reports are provided for every production batch, with support for third-party authoritative testing.
Parameter Category | Core Parameter | Standard Specification | Test Condition | Selection Reference |
|---|---|---|---|---|
Core Electrochemical Performance | Nominal Voltage | 3.2V per LiFePO4 cell / 3.7V per NCM cell | 25℃ room temperature | Customizable across 3.2V-800V range to match equipment requirements |
Core Electrochemical Performance | Energy Density | 90-160 Wh/kg | 25℃ standard charge/discharge | Suitable for weight-sensitive portable industrial equipment |
Core Electrochemical Performance | Cycle Life | ≥2000-5000 cycles @ 80% DOD | 25℃ 1C charge/discharge | Ideal for long-running energy storage applications |
Electrical Characteristics | Charge/Discharge Efficiency | ≥95% | 25℃ rated load | Reduces overall system energy consumption |
Electrical Characteristics | Self-discharge Rate | ≤3% per month | 25℃ open-circuit storage | Suitable for long-term backup power applications |
Electrical Characteristics | Continuous Discharge Rate | 1C-5C | 25℃ rated temperature rise | Supports high starting current requirements for industrial equipment |
Environmental Adaptability | Discharge Operating Temperature | -20℃ to 60℃ | Rated load | Works reliably in extreme outdoor temperature conditions |
Environmental Adaptability | Charge Operating Temperature | 0℃ to 45℃ | Standard charge current | Covers most industrial installation environments |
Mechanical Characteristics | Protection Rating | IP54 standard, customizable to IP67 | IEC 60529 test standard | Suitable for dusty, humid industrial field environments |
Note: The above parameters reflect standard series specifications. Customized parameter adjustments and function modifications are available to match special working condition requirements.
Core Technical Advantages
Compared to conventional industrial lithium battery packs on the global market, the product line delivers differentiated value through in-house R&D and production, validated through long-term industrial application with global clients:
1. High consistency and safety from in-house cell production: The company operates a fully automated cell production line with annual capacity exceeding 1 million units, holding multiple software copyrights and utility model patents for smart BMS technology. Cell capacity deviation is controlled within ≤2%, over-charge protection response time is less than 10ms, and thermal runaway trigger temperature is 30% higher than the industry average. This reduces battery maintenance frequency for industrial equipment, lowers safety accident risks, and extends the full lifecycle of battery packs.
2. End-to-end customization capability: The company provides full OEM/ODM development support, covering customized voltage, capacity, dimensions, BMS parameters, casing design and brand labeling. Sample development takes 3-7 days, bulk order delivery takes 15-30 days, with a standard minimum order quantity of 500 units. This reduces new product development cycles for clients, supports non-standard requirements for special industrial scenarios, and lowers supply chain coordination costs.
International Standards and Compliance
All R&D, design, production and testing processes follow the latest international standards and industry specifications, with a complete compliance and certification system to meet strict procurement and regulatory entry requirements for global clients. Core followed standards include IEC 62133 safety requirements for portable sealed secondary cells, IEC 62619 safety requirements for industrial lithium batteries, and UN38.3 test requirements for lithium battery transport. Product certifications include UL, FCC, CE, RoHS, UN38.3, MSDS, UKCA and CB, covering market entry requirements for North America, Western Europe, East Asia and Southeast Asia. Environmental compliance aligns with RoHS and REACH requirements. The company can provide factory inspection reports, third-party test reports and declarations of conformity to support client compliance audits.
Application Scenarios and Selection Guide
Selecting the appropriate industrial lithium battery pack model is critical to ensure application performance, stability and service life. The step-by-step selection process supported by the technical team includes: first, confirm core working condition requirements including rated voltage, capacity needs, operating temperature range, installation space dimensions, and target market compliance requirements; second, select the matching product series, choosing the high-energy-density NCM series for lightweight, high-power needs, or the high-safety LiFePO4 series for long-life energy storage needs; third, conduct sample validation, with free samples provided for real-world testing supported by one-on-one technical engineer guidance; fourth, confirm required compliance documents to match target market regulatory requirements; fifth, confirm customized requirements for non-standard dimensions or special BMS functions.
The product line is widely deployed across global industrial sectors, with two core high-value application scenarios:
1. Industrial power tools and portable equipment: The core industry demand is high-rate discharge, lightweight construction, vibration resistance and long cycle life. The adapted solution uses NCM lithium battery packs with high-rate cells and IP54 protective casings, applied to electric wrenches, industrial inspection equipment, drones and portable testing instruments. Verified client value includes 40% lower equipment weight, 60% longer single-charge runtime, and 2x longer maintenance intervals.
2. Commercial and industrial energy storage: The core industry demand is high safety, ultra-long cycle life, low self-discharge and stable output. The adapted solution uses LiFePO4 battery packs with smart BMS and modular design, applied to home energy storage, commercial backup power, communication station backup power and photovoltaic storage systems. Verified client value includes 5000-cycle service life, 50% lower full lifecycle cost, and 90% reduced thermal runaway risk.
FAQ
Q: Can you produce custom industrial lithium battery packs based on our specifications?
A: Yes, we support full customization of voltage, capacity, dimensions, BMS parameters, casing design and packaging to match your specific application requirements.
Q: What is your minimum order quantity for custom battery packs?
A: Our standard minimum order quantity is 500 units, with flexible adjustment for long-term cooperative clients and special project requirements.
Q: How long is the lead time for samples and bulk orders?
A: Sample orders are shipped within 3-7 days, bulk orders are delivered within 15-30 days depending on order volume.
Q: Do your products meet global market compliance requirements?
A: Our products hold UL, FCC, CE, RoHS, UN38.3, UKCA and CB certifications, meeting entry requirements for North America, Western Europe, East Asia and Southeast Asian markets.
Q: What is the warranty period for your industrial battery packs?
A: We provide 1-3 years of warranty for all battery packs, with remote technical support and core component replacement services for end users.
Contact Us
Official Website: https://www.zfchuntbattery.com/
Email: [email protected]
Global Service Hotline: 8613662889755
Factory Address: Building 2, Phase II, Yuyang Science Park, No.107 Fenggang Section, Dongshen Road, Fenggang Town, Dongguan City, Guangdong Province, China.
Previous:What Is the Customization Capability of Chinese OEM Nickel Metal Hydride Batteries
Next:How to Source Reliable Industrial Lithium Battery Packs from Chinese Wholesale Manufacturers
Guess You Like
-
How to Source Chinese OEM Emergency Start Battery Supply A Practical Guide
This guide is compiled by senior battery engineering managers from Shenzhen Kangkedi Intelligent Technology Co., Ltd., a leading new energy battery solution provider, to address the most common pain p
-
How to Source Reliable Industrial Lithium Battery Packs from Chinese Wholesale Manufacturers
This guide is compiled by the senior technical team of Shenzhen Kangkedi Intelligent Technology Co., Ltd. (global brand ZFCHUNT), a leading integrated industrial lithium battery manufacturer with year
-
China Original Source Industrial Lithium Battery Packs Technical Overview Compliance Standards
This technical article provides a comprehensive, standards-aligned overview of industrial lithium battery packs, independently developed and manufactured by Shenzhen Kangkedi Intelligent Technology Co
-
What Is the Customization Capability of Chinese OEM Nickel Metal Hydride Batteries
This technical article provides a standardized interpretation of OEM nickel-metal hydride (NiMH) battery customization capabilities, developed and manufactured by Shenzhen Kangkedi Intelligent Technol
-
How to Solve Global Automotive Battery Sourcing Pain Points with Chinese OEM Automotive Battery Foreign Trade Service Providers A Practical Guide
This guide is compiled by the senior technical manager of Shenzhen Kangkedi Intelligent Technology Co., Ltd., a leading new energy battery solution provider with 10+ years of R&D and manufacturing
-
Chinese OEM Battery Sample Suppliers How to Source Reliable Partners
This guide is compiled by senior battery R&D engineers from Shenzhen Kangkedi Intelligent Technology Co., Ltd. (global brand: ZFCHUNT), a leading new energy battery solution provider with years of
-
China Outdoor Energy Storage Lithium Battery Technical Solutions for Global Trade
This article provides a standardized technical overview of outdoor energy storage lithium batteries, independently developed and manufactured by Shenzhen Kangkedi Intelligent Technology Co., Ltd. (glo
-
Outdoor Energy Storage Lithium Battery Solutions A Complete Guide for Global Buyers
This guide is compiled by the technical team of Shenzhen Kangkedi Intelligent Technology Co., Ltd. (global brand ZFCHUNT), a leading Chinese cooperative service provider of outdoor energy storage lith
-
Technical Overview of OEM Drone Battery Solutions from Chinese Manufacturers
This article provides a technical interpretation of OEM custom drone lithium battery solutions, independently developed and produced by Shenzhen Kangkedi Intelligent Technology Co., Ltd. (global brand
-
Chinese Cost Effective OEM Battery Suppliers How to Solve Global Sourcing Pain Points
This guide is compiled by Shenzhen Kangkedi Intelligent Technology Co., Ltd., a new energy lithium battery OEM/ODM solution provider, with input from our core team of senior engineers with 10+ years o
